You are using an out of date browser. It may not display this or other websites correctly.
You should upgrade or use an alternative browser.
You should upgrade or use an alternative browser.
My 50cal miniture BP cannon
- Thread starter gnmontey
- Start date


Op do you have a drawing/blieprints of it or something? I want to do something similar.
No plans, sorry. I posted here for plans and searched and searched the internet for plans and came up empty handed for the most part.
I have a few full size cannon specs I can send you. Too elaborate for my meager machining skills.
You can try these but I think they are for display only. http://www.tvdsb.ca/webpages/hoefnagelsd/cannon_drawing.cfm
Poke around that website there are a couple plans there.
I can PM my dims if that helps. The contours were pretty much free lance (sort of) after I got through the boring ordeal, and I left lots of meat in the breach area. Also, I mounted the trunnions too far back, it's bbl heavy.
I started this project with this https://www.princessauto.com/en/detail/1-1-4-in-diameter-x-7-in-long-cylinder-pin/A-p3800445e
Please be advised that I have not proofed this thing yet. I'm thinking along the lines of 50gn FF and a 50cal RB Max.
M
Last edited:

How the heck do you do that? Turn a series of steps and then taper each step?
I have been tempted to try the offset tail stock technique but can't get my head around how one ends up with a symmetrical piece in the end.
I turn the cross feed so that it is almost parallel to the bore of the cannon barrel and is angling away from the bore at somewhere between 0.5 and 1 degree. Essentially I know what diameter I want at the small end and what I want end up with on the other end and adjust the angle of the cross feed to achieve that. I also lock the carriage in place with the half nut on the longitudinal feed. I cut a taper for about 2" or however far my cross feed will travel then move the carriage ahead and repeat. What Guntech is suggesting is to have a offset center mounted in your tail stock, centered in the muzzle and use a faceplate and dog assembly instead of a chuck and have a dead center in the head stock as well. The reinforces are the decorative bands that you see on some cannon barrels. By the time that cannon barrels were cast, I think those bands were mostly decoration
cheers mooncoon
fingers284
CGN Ultra frequent flyer
- Location
- Alberta Cowboy Ranges
I turn the cross feed so that it is almost parallel to the bore of the cannon barrel and is angling away from the bore at somewhere between 0.5 and 1 degree. Essentially I know what diameter I want at the small end and what I want end up with on the other end and adjust the angle of the cross feed to achieve that. I also lock the carriage in place with the half nut on the longitudinal feed. I cut a taper for about 2" or however far my cross feed will travel then move the carriage ahead and repeat. What Guntech is suggesting is to have a offset center mounted in your tail stock, centered in the muzzle and use a faceplate and dog assembly instead of a chuck and have a dead center in the head stock as well. The reinforces are the decorative bands that you see on some cannon barrels. By the time that cannon barrels were cast, I think those bands were mostly decoration
cheers mooncoon
I think you are referring to the "top-slide" are you not. The cross feed is anchored permanently at a right angle to the carriage. To cut a taper with the cross slide you would have to operate the cross slide feed dial at the rate of taper while the carriage is fed along the length of the work piece.
No plans, sorry. I posted here for plans and searched and searched the internet for plans and came up empty handed for the most part.
I have a few full size cannon specs I can send you. Too elaborate for my meager machining skills.
You can try these but I think they are for display only. http://www.tvdsb.ca/webpages/hoefnagelsd/cannon_drawing.cfm
Poke around that website there are a couple plans there.
I can PM my dims if that helps. The contours were pretty much free lance (sort of) after I got through the boring ordeal, and I left lots of meat in the breach area. Also, I mounted the trunnions too far back, it's bbl heavy.
I started this project with this https://www.princessauto.com/en/detail/1-1-4-in-diameter-x-7-in-long-cylinder-pin/A-p3800445e
Please be advised that I have not proofed this thing yet. I'm thinking along the lines of 50gn FF and a 50cal RB Max.
M
What did you do for a powder pocket?
I think you are referring to the "top-slide" are you not. The cross feed is anchored permanently at a right angle to the carriage. To cut a taper with the cross slide you would have to operate the cross slide feed dial at the rate of taper while the carriage is fed along the length of the work piece.
I stand corrected.
cheers mooncoon
What did you do for a powder pocket?
"Powder pocket"? What's that? None of the full size cannon drawings I looked at showed anything unusual in the breech area.
M
Last edited:
fingers284
CGN Ultra frequent flyer
- Location
- Alberta Cowboy Ranges
Some BP cannons did have a "smaller than bore" powder chamber, they were refereed to as "howitzers". Made either by a " bore form" with a smaller section at the end big enough to hold a pre-determined powder charge or just by simply counter boring it in after casting. From what I can gather from reading that the Howitzer chambered guns were mostly of the lighter weight (cavalry) guns and it allowed "extra" metal thickness at the breech without the added weight that a reinforcing ring would add.
One of the cannons I built has a "smaller than bore" chamber area and it is somewhat more difficult to get the powder charge to seat properly... I need a "false bore" pipe that holds the powder until it is up against the chamber and another rod to seat it where it can be accessed by the fuse. A lot of screwing around that the old-timers didn't mess with...they didn't use foil-wrapped powder charges, just poured loose powder.
One of the cannons I built has a "smaller than bore" chamber area and it is somewhat more difficult to get the powder charge to seat properly... I need a "false bore" pipe that holds the powder until it is up against the chamber and another rod to seat it where it can be accessed by the fuse. A lot of screwing around that the old-timers didn't mess with...they didn't use foil-wrapped powder charges, just poured loose powder.
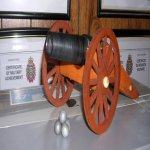

Make suer when u do fire it leave the carriage loose to recoil as it will If u tie it down the carriage will disintigrate
I hear you on that one. I figure the order of failure is as follows.
1. Carriage disintegrates.
2. Trunnions let loose.
3. BBL, but I'm kind of doubting that. Lot's of meat in the breach area.
Contemplating adding some lead to carriages just to keep the whole thing from becoming a projectile.
M
- Location
- vancouver island
A thought for you on powder charge. Really the piece is a pistol fired by a fuze so as with muzzle loader pistols about 1/2 your caliber should be your charge-hence, about 25 grains fffg. This is what I use in mine with fairly good results. As for sighting-the fuze is the rear sight and a filed notch at the muzzle centered on the bore is the front. Elevation is by guess and by God. Cheers,