Problem with .32 rimfire cases

guninhand

CGN frequent flyer
Rating - 100%
88   0   0
Location
East Coast
I got machined .32 rimfire cases from DGW and the recommended blank primers, 6mm Dynamit Nobel, seat 0.01 inch proud. This prevents loading in my antique revolver. I tried another blank .22, Simpson brown .22 for concrete, and it's only 0.0017" proud, still too high. Only perfectly flush (or even a little deeper) primers will work. Looking for suggestions to deepen the primer pocket in the machined cases. I suspect taking them to a machinist would be cost prohibitive. Any ideas?

notflush_zps5281b291.jpg
 
Try .22 Short cases with the bullet pulled.

Might be possible to deepen the rim seat with a .22 chambering reamer.
 
I use START 6
22 rf blanks there Dia is smaller than some 22 rf blanks but there rim depth seems to be good .
what gun are you useing ? most have enough head space to clear them even ones sticking up abit higher.

A milling machine with the right bit / cutter is the way to go to alter them.
 
The rims are too thick on the machined cases. When I was making them they had to be about .015" thick in the cases or less and chamferred to work in all guns. The pics you have show them being far to thick. You chould probably take off a few thou with some emery cloth though.
 
Tac870, the rims are 0.055 inch. They are a slip fit in the cylinder/cylinder face gap. I would have to take off brass from the side of the rim that faces the case mouth to get the primers to fit.
marlinantique_zps71166bb6.jpg


Dingus, the gun is a Marlin. What is START 6? Couldn't find it with Google.

Tiriaq, remington .22 shorts protrude only 0.0014 inch. Still too much. I'll have to track down someone with a .22 reamer.
 
I have made several calibers of rimfire cases and I make the rims about .005 or so thin and cut a rim recess in the outer shell that lets the blank shell or the hilti sit roughly the same amount proud. Otherwise you will find that the outer brass rim will be absorbing energy and resulting in a softer blow on the blank or on the hilti shell. I think in your case, unless you can think of a way of removing metal from the front of the rim of the outer shell, you would be better off thinning the rim from the back and then cutting a correspondingly deeper rim recess for the blank. Ultimately you want the blank to sit proud and the total rim thickness of both shells to be within the tolerances of your gun

cheers mooncoon
 
The rims are too thick on the machined cases. When I was making them they had to be about .015" thick in the cases or less and chamferred to work in all guns. The pics you have show them being far to thick. You chould probably take off a few thou with some emery cloth though.

He is right they look way thicker than the ones i use take the metal off the forward side of the rim that will let the 22 Rf blanks work as that will alow the cases to move forward takeing the blanks forward with the case.
A small lathe could do that easy.
 
I don't have a lathe, but I might be able to do it on my drill press. The case mouth takes a pencil as a slip fit so I could use that for the arbor to grip the mouth and not crush anything, then have the base in a fixed, pre-aligned aluminum bar with a shallow hole to secure half the case rim, and remove the forward half with a file as the case turns. I didn't realize how unnecessarily thick the rim is.
 
He is right they look way thicker than the ones i use take the metal off the forward side of the rim that will let the 22 Rf blanks work as that will alow the cases to move forward takeing the blanks forward with the case.
A small lathe could do that easy.

Are you still using the ones I made for you?
 
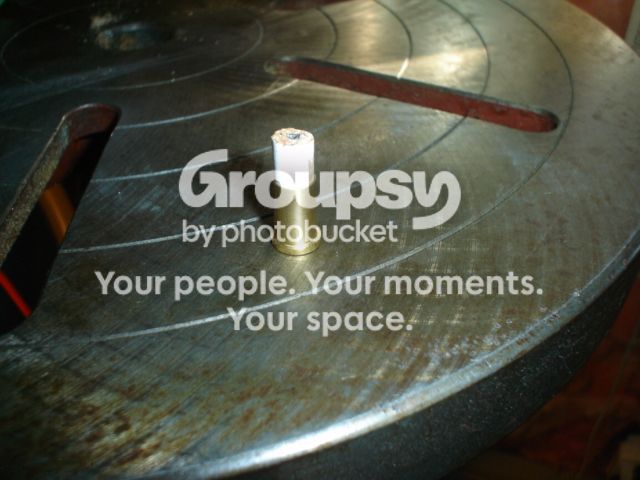
I went ahead to fix the cases and it worked, so here's what I did. First I put a pencil stub in the case mouth to prevent crushing.
rf1_zpse2ad3e94.jpg


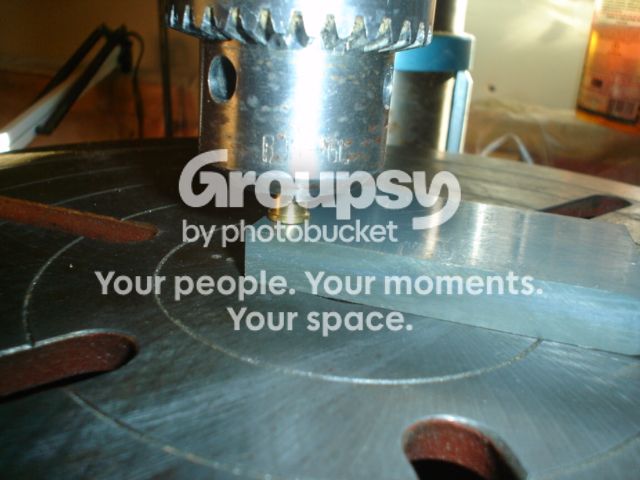
Then I put the case up into the chuck of the drill press and placed a stable flat block under it. Then with the case resting on the block tightened the chuck by hand, and pulled the block away. Now I had a system where the case is the same precise distance from the drill press table every time.

rf2_zps8c440cdc.jpg


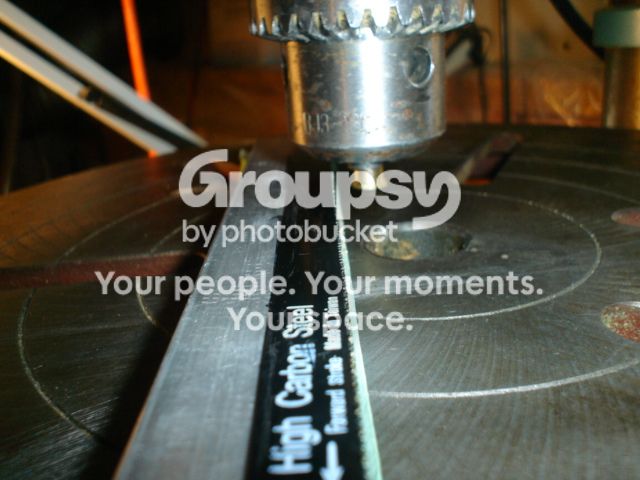
Then I got a rectangular metal rod of appropriate height and fine tuned total height by adding strips of painter's masking tape to the bottom.

rf3_zpsebfa91b4.jpg


So holding a hacksaw blade on top, and the drill press turned on, it was quick and easy to just slide it in and remove material from the top part of the rim. The height of the cutter is the same every time. Just have to be careful and watch closely not to cut into the body of the case. The results were perfect. Case rims are now all about 0.044 inch thick and when .22rf blanks are inserted there is 0.006 in. clearance with the back part.

fr2_zps3de716ad.jpg


All I have to do now is anneal the cases and I have 475 deg temilaq for that. Also have dead soft commercial buckshot and FFFg. Anyone know if the gun can handle .32 long as well?
 
Last edited:
Back
Top Bottom